When comparing platinum silicone vs tin silicone for mold making, both systems can produce flexible molds with detailed surfaces. Their curing chemistry creates different limits around contamination, dimensional stability, contact requirements, workshop control, and long-term production planning. When clean curing and controlled dimensions carry high project value, Platinum Cure Silicone often enters the first material review. Review BK-A platinum-cure silicone in Shore A5 and A15 when comparing material options for a mold-making project.
A catalyst name alone cannot approve a mold-making material. The master pattern, casting media, dimensional tolerance, contact conditions, workshop history, production frequency, and available documents must support the choice. Tin-catalyzed material may remain practical for general casting, decorative reproduction, temporary tooling, or uncertain master surfaces.
How Platinum Cure and Tin Cure Systems Differ
Addition-cure silicone uses a platinum catalyst to form the cured elastomer. The reaction does not depend on releasing a curing byproduct. This chemistry often receives early consideration for molds that need stable geometry, clean processing, or controlled production conditions.
Tin-catalyzed silicone uses condensation-cure chemistry. During crosslinking, the system releases a small-molecule byproduct. That difference can influence odor, dimensional behavior over time, storage planning, and compatibility with certain casting materials.
Chemistry describes a material family rather than every grade. Hardness, viscosity, tear behavior, working time, cure conditions, color, and intended application can vary within either system. The final comparison should use the current TDS for the exact grades under review.
| Decision point | Platinum / Addition Cure | Tin / Condensation Cure |
|---|---|---|
| Typical direction | Precision cavities, repeated production, stored mold libraries, and projects where clean curing or controlled dimensions matter. | Prototypes, decorative molds, general casting, temporary tooling, and some projects with uncertain master surfaces. |
| Main caution | Sulfur, latex, tin residues, some amines, and certain resin surfaces can interrupt the cure. | Curing byproducts and possible dimensional movement should enter the review. |
| Before approval | Confirm grade documents and test the actual master, coatings, release system, tools, and cure environment. | Confirm grade documents and test the actual casting process, dimensions, storage needs, and demolding conditions. |
Neither family is automatically superior. Addition curing can fail against an incompatible master, while dimensional movement can make tin curing costly for fitted parts. The correct route controls the most expensive and most likely project risk.
Comparison by Project Decision Factors
A useful review connects each requirement to a production consequence. Dimensional stability, curing cleanliness, contact documentation, durability, storage, workshop control, and total cost should be considered together. Otherwise, one attractive property can hide a larger operational problem.
Dimensional stability. Addition-cure systems generally receive stronger consideration when molds must retain controlled geometry. Since the cure does not create a condensation byproduct, one source of later dimensional movement is removed. This becomes more valuable for fitted components, repeated masters, and molds that return to service after storage.
Odor and curing cleanliness. Addition curing avoids the byproduct associated with condensation chemistry. This can simplify process planning where odor, residue, or clean handling matters. A tin-cure system may need closer attention to cure completion and compatibility with the next casting material.
Contact requirements. Food-related and specification-controlled molds need evidence for the exact grade. Catalyst chemistry alone cannot confirm suitability for every market, media, or repeated-use condition. Product identity, document revision, test scope, and processing instructions should align before production approval.
Durability and handling. Mold life depends on undercuts, thin lips, casting temperature, abrasive fillers, release force, cleaning, storage, and support design. Addition-cure material often enters repeated production because stable geometry may reduce replacement risk. Tin systems can still suit shorter campaigns or less demanding shapes.
Material cost. Tin-catalyzed silicone may reduce the initial expense for temporary tooling, large decorative molds, or early prototypes. Addition-cure material may justify a higher budget when it controls a specific dimensional or process risk. Testing, scrap, tool separation, storage, and replacement should therefore enter the comparison.
Storage and site control. Unopened storage, opened-container handling, humidity exposure, and temperature limits should come from current technical documents. Platinum-sensitive work may need dedicated containers, stirrers, gloves, scales, and surfaces. In a mixed workshop, this separation may decide whether the process stays repeatable.
How Application Requirements Change the Material Decision
These finished mold examples show why the same silicone family cannot be selected from one property alone. Food-detail work places more weight on contact documentation and clean release, while plaster or cement casting adds structural support, abrasion, and demolding load to the review.
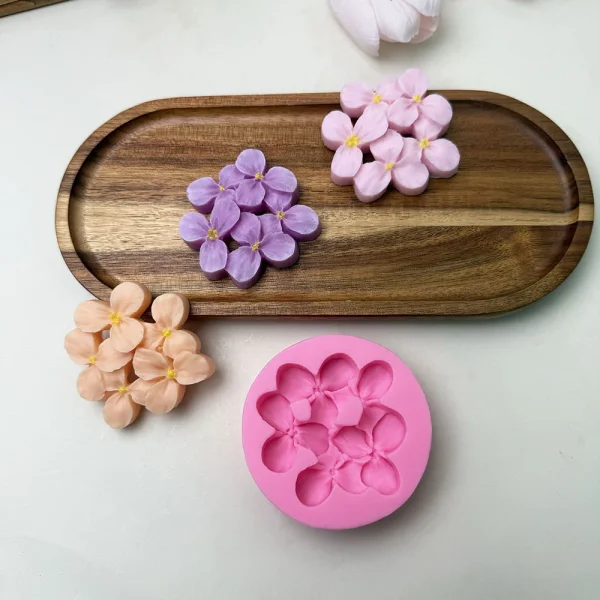
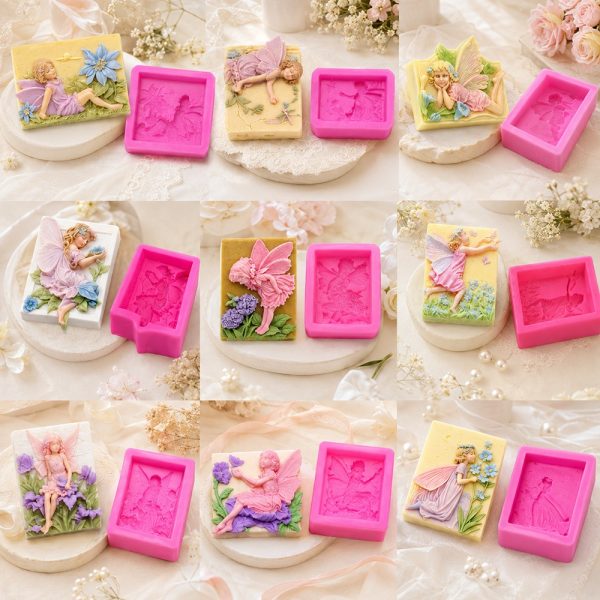
Selection point: these products illustrate application differences; they do not replace grade-level review. Master compatibility, casting media, dimensional tolerance, production frequency, and current technical documents should still control the material choice.
Browse Silicone MoldsCure Inhibition Risk
Cure inhibition occurs when a contaminant interferes with the platinum catalyst. The silicone may remain liquid, feel tacky, cure unusually soft, or fail only at the master interface. Sometimes the main body cures while a thin boundary layer remains uncured.
A small compatibility test becomes essential whenever the master composition or workshop history remains uncertain. The test should include the planned sealer, release agent, pigment, tools, gloves, and cure environment. A clean cup test confirms bulk curing, but it does not confirm contact compatibility.
Six red flags before a full mold pour
Sealing may reduce inhibition on some masters, although the coating creates another variable. It can change texture, gloss, fine detail, or release behavior. Incomplete coverage may also leave isolated tacky areas around narrow features.
A useful test applies a small mixed batch to a representative area of the final master. After the documented cure period, the interface should be checked for tack, softness, transfer, and missing detail. The record should include material batch, surface preparation, ambient conditions, and cure observations.
When a test fails, only one variable should change at a time. Replacing the gloves, sealer, clay, and container together may produce a successful second test, but the original cause remains unknown. Controlled troubleshooting creates a process that production can repeat.
Casting Material and Application Fit
Casting media can change the preferred silicone direction. Food-related mixtures, wax, polyurethane, epoxy, plaster, concrete, and industrial compounds place different chemical and mechanical loads on a mold. Testing should therefore use the actual production formula rather than a broad material label.
Food and confectionery applications. Food-related molds need documented suitability for the exact grade and intended market. Addition-cure chemistry often enters the first review, yet catalyst type alone cannot replace current evidence. Pigments, cleaners, release agents, post-cure instructions, and repeated-use conditions should also align.
Wax and candle casting. Both silicone families can support wax casting when hardness and geometry match the design. Tin-cure material may suit development runs, while addition-cure material may offer more value for repeat production or mold storage. The trial should include the planned wax, fragrance, dye, and pouring method.
Polyurethane, epoxy, and polyester resin. Resin casting can expose a mold to chemical stress and curing heat. Compatibility should be checked with the exact resin, hardener, pigment, filler, and release system. Trials should examine both the casting surface and the mold after demolding.
Plaster and gypsum. These materials can work with either silicone family. Tin-cure material may be economical for decorative work, while addition-cure material may suit detailed duplication or stored mold libraries. Mold size, surface texture, handling, and the support shell still affect cavity shape.
Concrete and cement-based casting. Concrete creates weight, abrasion, alkalinity, and high demolding force. As a result, geometry and support often dominate the decision. A realistic trial should reproduce the aggregate, additives, support shell, and planned handling method.
Industrial prototypes and fitted components. These parts may include mating surfaces, controlled wall sections, or inspection points. Stable geometry can therefore outweigh the lowest material price. However, sulfur clay, mixed coatings, or an uncertain resin print may make a tin-cure route safer during early development.
Production Volume and Mold Life
Production volume should be defined as a planning range, not an unsupported casting count. Mold life changes with casting chemistry, pouring temperature, undercuts, wall thickness, release force, cleaning, storage, and handling. A universal cycle claim cannot replace project testing.
A prototype used once has different priorities from a mold stored for scheduled repeat orders. The cost of replacing a simple decorative mold also differs from replacing a qualified assembly mold. Production frequency should influence both the material decision and the depth of validation.
Development and short campaigns
Early work often prioritizes practical compatibility, manageable cost, and fast learning. Tin-cure material may fit when long storage and tight dimensions have limited importance.
An assembly prototype can still require high accuracy. In that case, an addition-cure grade may be justified after a successful inhibition test.
Repeated and scheduled production
Repeat work places more value on storage stability, predictable dimensions, and consistent demolding. An addition-cure grade may provide stronger commercial value under those conditions.
However, poor geometry can shorten life in either system. Thin edges, trapped undercuts, and unsupported walls should be corrected before chemistry receives the blame.
A qualification plan can examine detail reproduction, demolding force, part dimensions, mold recovery, and visible damage. It should also record casting temperature, release method, cleaning, and storage between casts. These records show whether the process remains stable beyond one successful casting.
The plan does not need an invented lifetime guarantee. Instead, it can define an initial validation stage and inspection points during production. This approach keeps mold-life decisions connected to actual operating conditions.
Dimensional Accuracy and Shrinkage
Dimensional accuracy begins with the master. Master tolerance, coating thickness, mold-box rigidity, mixing quality, cure environment, support structure, and measurement method all affect the final cavity. Catalyst chemistry matters, although it remains one part of the dimensional chain.
Addition-cure systems generally receive stronger consideration for long-term dimensional control. Condensation-cure molds may show more movement as curing byproducts leave the material. The actual result should be confirmed through grade documents and measured samples rather than a percentage copied from another formulation.
Why small changes matter. A decorative object can tolerate minor variation without a visible problem. However, lids, inserts, housings, seals, and mating parts may not. A small cavity shift can affect alignment, wall thickness, or assembly force.
Multi-part molds and registration. Multi-part molds rely on stable parting surfaces and accurate registration features. If one section moves, flash lines and assembly mismatch can increase. The mold jacket and clamping method must hold every section in a repeatable position.
Hardness and support. A soft cavity can deform under resin weight, concrete pressure, or excessive clamping. For precision work, hardness and support design should be reviewed together. The most stable chemistry cannot compensate for a cavity that moves under load.
Measurement strategy. Critical dimensions should be identified before mold making begins. The master, cured cavity, and sample casting can then be checked at the same points under consistent conditions. For important assemblies, a checking fixture may provide clearer evidence than isolated measurements.
Cost Beyond Material Price
Material price is easy to compare, but it may represent only one part of project cost. Failed cure, discarded masters, contaminated tools, repeat pouring, rejected castings, production delays, and dimensional problems can exceed the silicone expense.
The commercial review should examine the complete workflow. A lower-cost system can be economical for a temporary decorative mold. A higher-cost system may be more efficient when it removes a specific risk that would otherwise create scrap or rework.
Include these costs in the comparison
- Master cleaning, sealing, and compatibility testing
- Rejected silicone, mold-box materials, and lost labor
- Dedicated tools and contamination-control procedures
- Finished-part scrap caused by distortion or surface defects
- Mold replacement after storage or repeated production
- Document review, incoming checks, and sample qualification
An inhibited mold may require complete replacement. The loss can include silicone, master preparation, labor, mold-box materials, and delayed casting. A small contact test can protect a much larger investment.
A mold may also cure correctly yet produce unusable parts. Distortion, surface contamination, seam mismatch, missing detail, and demolding damage can increase scrap. Qualification should therefore examine the finished casting as well as the mold.
Documentation carries value in specification-controlled work. Current technical files, batch identity, incoming checks, and retained test records improve traceability. The grade name, revision date, and supplied material should align before production release.
Decision Matrix
The following matrix provides an initial direction rather than final approval. Each scenario still needs grade-specific documents, representative materials, and realistic process testing. When several risks overlap, the test result should lead the decision.
Custom Project or Ready-Made Mold?
Some projects need raw material and an internal mold-making process. Others need a finished mold with the parting strategy, support structure, and demolding route already resolved. Defining that boundary early prevents an incomplete purchase brief.
Material supply is the clearer route when
- A usable master and mold-box method already exist.
- Weighing, mixing, and curing can be controlled internally.
- Tools can remain separated from known inhibitors.
- A compatibility test can be completed before the main pour.
A finished custom mold is the clearer route when
- The parting line or support structure is not defined.
- The master needs compatibility or manufacturability review.
- Undercuts or fragile details make demolding uncertain.
- A production-ready mold is required instead of raw material.
Questions to Ask Before Buying
A useful inquiry should describe the master, casting media, critical dimensions, process environment, contact requirements, and production frequency. The exact grade documents should be requested at the same time. Clear inputs allow a material comparison without inventing performance assumptions.
Define pass criteria before testing. Useful checks include interface cure, detail reproduction, demolding force, dimensional accuracy, casting compatibility, surface finish, and visible mold damage. Without defined criteria, a sample may look acceptable while missing the main production risk.
A successful cup test confirms that the two silicone components can cure together. However, it does not validate the master surface or casting material. A complete qualification plan should cover both chemical compatibility and structural performance.
Frequently Asked Questions
What is the main difference between platinum cure and tin cure silicone?
The main difference is the crosslinking chemistry. A platinum-catalyzed material uses addition curing and does not release a curing byproduct. A tin-catalyzed material uses condensation curing and releases a small-molecule byproduct during crosslinking.
That difference can affect contamination sensitivity, dimensional behavior, odor, storage, and casting compatibility. Even so, each grade needs a current TDS and a representative sample.
Which silicone is better for food-contact molds?
An addition-cure grade often receives stronger consideration because the reaction avoids condensation byproducts. Nevertheless, catalyst chemistry alone does not confirm food-contact suitability.
The exact grade needs relevant documents for the intended market and conditions. Pigments, release agents, cleaners, and post-cure instructions should also enter the review.
Why can platinum silicone fail to cure?
Certain substances can interfere with the catalyst. Common concerns include sulfur-containing clay, natural latex, tin-cure residue, some amines, and incompletely prepared resin prints.
The failure may appear as tackiness, softness, or an uncured interface. A small test using the actual master, sealer, release agent, and workshop tools can identify the risk before full production.
What documents should be requested before ordering?
The core documents include the current TDS and SDS for the exact grade. Where contact or performance claims matter, relevant existing test information should also be reviewed.
Batch identity, storage guidance, mix ratio, cure conditions, known inhibitors, and sample availability support a reliable decision. Missing figures should remain unconfirmed until suitable evidence becomes available.
Final Selection
The final choice should balance master compatibility, casting media, accuracy, workshop control, production frequency, and total cost. The lowest material price should be weighed against failed cure, scrap, rework, and mold replacement.
Three actions make the decision more reliable:
- Map every material that touches the silicone, including the master, coatings, tools, gloves, and release agents.
- Define pass criteria for cure quality, dimensions, demolding, surface finish, and casting compatibility.
- Review current documents and complete a representative sample before a large mold pour.
Submit Real Project Conditions for Material Review
A useful review should include the casting material, master material, contact requirements, critical dimensions, workshop contamination risks, target production range, and main budget priority. BKSilicone can then compare material directions without assuming price, MOQ, lead time, certification, mold life, or unverified performance.
For addition-cure material evaluation, include the actual master and casting conditions when asking about Platinum Cure Silicone.